Thousand-litre aseptic filler
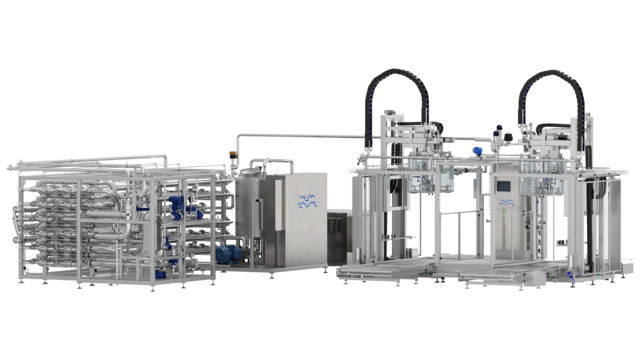
Transfer sterile food products and beverages into bag-in-box packaging, drums, totes and bins with the Alfa Laval Thousand-litre aseptic filler (TAF). It helps safeguard product integrity – from filling to final use – while minimizing contamination risks and product losses. Designed for reliable, efficient operation, this plug-and-play drum, tote and bin filler helps reduce operating and maintenance costs, maximize uptime and boost productivity.

Drum, tote and bin filler boosts productivity, flexibility and product safety
- Keep production running with high uptime, precise and repeatable filling, and reliable performance throughout the filler lifecycle.
- Clean with confidence. Achieve faster, easier and more reliable automatic cleaning and sterilization while minimizing cleaning-in-place downtime.
- Improve operator safety, accessibility and ergonomics with easier access for operation, inspection and maintenance.
- Adapt capacity and configuration as production requirements evolve, with a modular platform designed for future expansion.
- Start producing sooner with fast, easy installation and commissioning with a modular, plug-and-play approach.
Optimize aseptic filling across applications, from prepared foods and beverages for consumers to bulk food ingredients for industrial processing. The Alfa Laval Thousand-litre aseptic filler helps protect product integrity during filling, storage and transport, supporting safe, high-quality products through to final use.
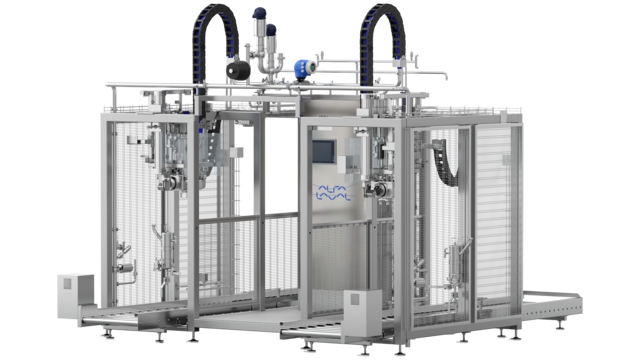
Combining precise filling, hygienic design and packaging flexibility, this servo-driven aseptic filling equipment handles liquid and highly viscous food products containing particles. Designed for 1,000-litre bags in palletizable containers, this aseptic bag-in-bin filler also supports efficient bulk filling into totes, bins and drums.
An automatic, hands-off cleaning procedure and fully drainable design enhance operational safety and hygiene. Servo motor cylinders with encoder feedback improve reliability and stability, helping reduce maintenance costs. An aseptic sterile intermediate cleaning mode enables longer production runs between cleaning cycles, increasing uptime and overall productivity.
Modular, versatile and easy to upgrade, the TAF delivers rapid and accurate filling of liquid food products and highly dense, viscous low-acid products containing particles. Optional equipment, multiple filling heads, semi-automatic and automatic operation, and accessories help you adapt to changing production needs.
Available packaging configurations include 3–20-litre bags, 220-litre bag-in-drums, and four 220-litre bag-in-drums on pallets. Additional configurations are available for selected bag-in-box aseptic fillers and bulk packaging applications, including aseptic bag-in-bin filler applications. The TAF can also be configured as a tote filler to suit specific production requirements.
How does the Thousand-litre aseptic filler work?
Choose between semi-automatic and automatic filling modes to suit your production requirements. This drum, tote and bin filler supports reliable, large-volume filling.
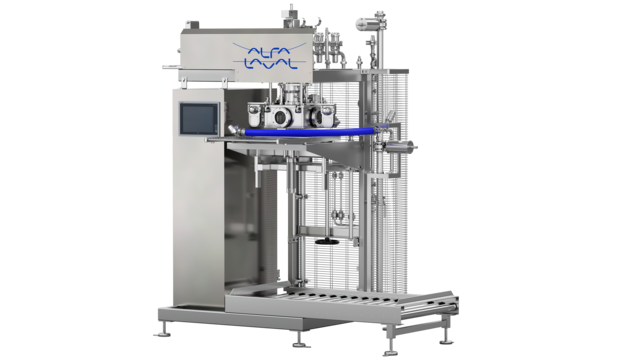
Semi-automatic filling: The operator inserts the bag neck into the filling head, initiating an automatic sequence that opens, fills and closes the bag. During filling, the temperatures of the steam barriers and filling valve are monitored and controlled to help maintain aseptic conditions.
For 1,000-litre bags, the filling head moves into the downward position to distribute the product evenly, particularly when filling viscous products, and help prevent folds from forming in the bag corners.
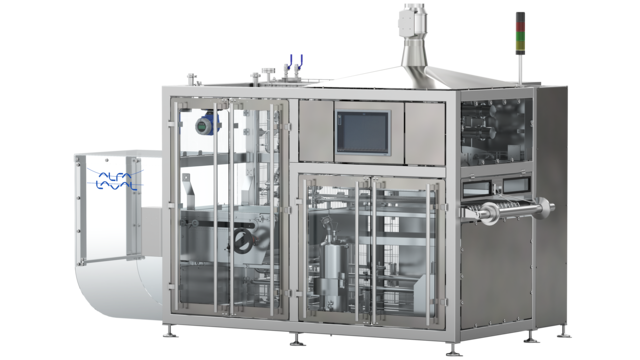
Automatic aseptic filling: An optional automatic bag feeder (ABF) for 3–20-litre bags manages bag loading, cap opening, filling and cap closing, reducing the need for operator intervention.
Contact Alfa Laval to discuss your aseptic filling requirements and find the right configuration for your production needs.
Aseptic bins filler
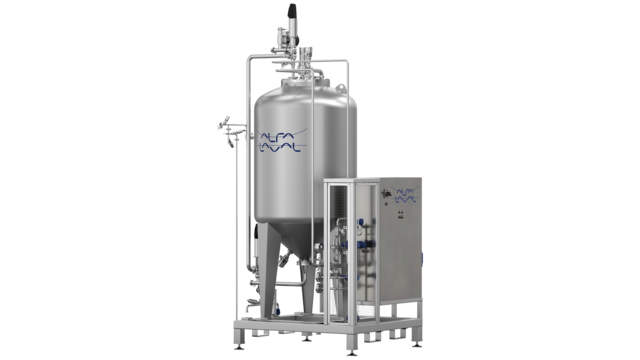
Steritank aseptic tank
Automatic bag loader (ABF)
Products
Food system services
Alfa Laval Food system services help extend the performance of your food systems by maximizing the performance of your processes. This enables you to:
- Continually improve your operations to maintain competitive advantage
- Focus on uptime, optimization and availability
- Maximize return on investment throughout the life cycle of your food systems
Learn more about our service offer for food systems